Product Description
Fits: GM Powerglide (aluminum)
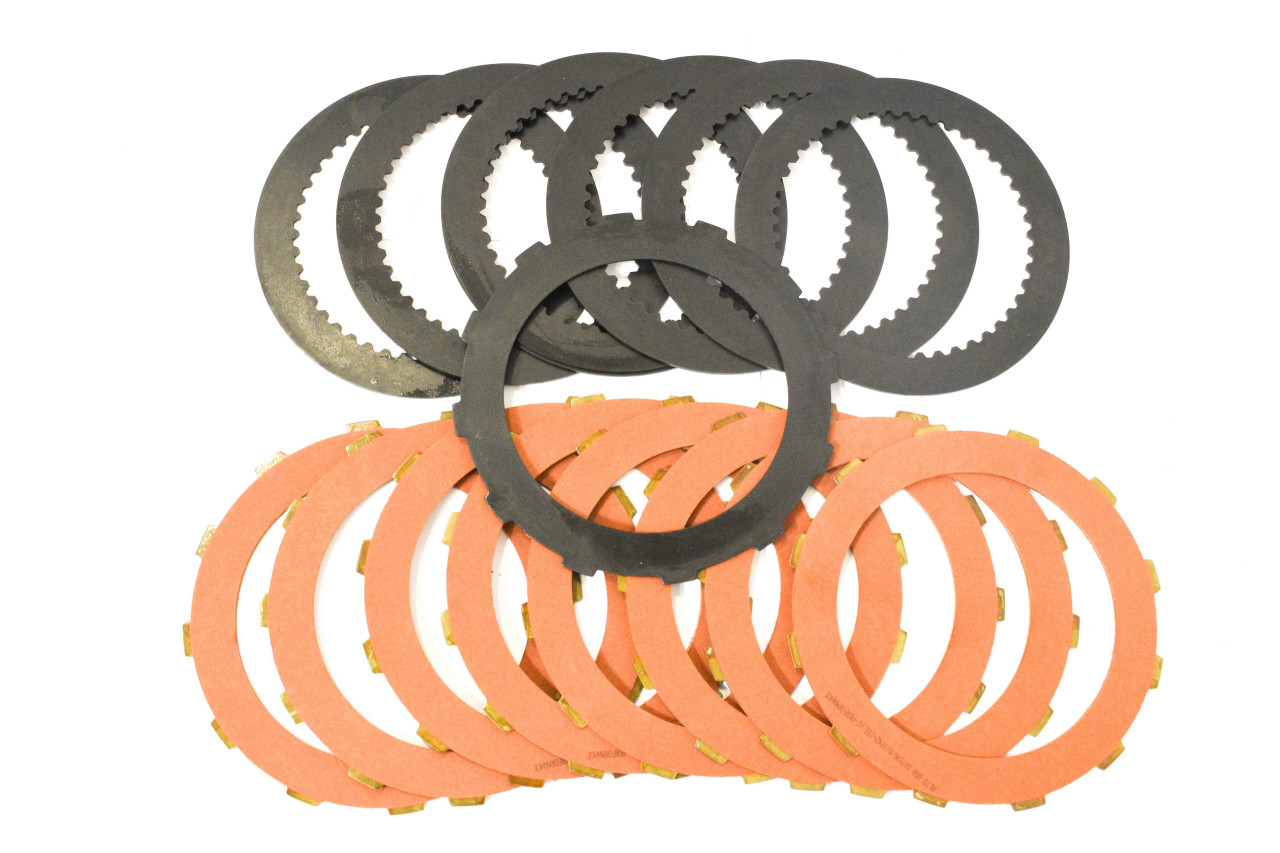
High clutch PowerPack for building an aluminum GM Powerglide for high-performance and racing use, made in the USA by Alto Products Corp. The friction plates are Red Eagle® high-performance paper with external teeth, and the Kolene® coated steel plates have internal teeth. With the steels splined to the turbine shaft and the frictions splined to the front drum, the high gear shift is much firmer and shorter.
Specifications
| Clutch | High |
|---|---|
| Piston height after machining | .745” (+/- .005) |
| Clutch pack clearance | .080 +/- .010 (min/max .060-.100) |
| Made in | USA |
| Alto part number | 019756 |
Installation
The plates are selectively sized (thinner) to fit the full capacity of eight (8) friction plates. First measure from the bottom of the clutch drum (the area under the bottom of the piston) to the sun gear flange ledge, about 3/16” below the snap ring groove. The measurement should be approximately 1-7/8 (1.875); it is much shorter with a six-cylinder drum.
Piston: there are three (3) curved, bathtub-shaped pads on the bottom side of the piston. Machine the piston from the top of area “A” (where the first steel plate rests) until the height is .745” (+/- .005).
Plates: install the piston seals, piston, return springs, spring retainer and retainer snap ring. Start with one of the flat steel plates with external teeth, then a friction plate, and continue alternating in the usual manner; the top plate is a friction. Presoak the friction plates in clean ATF for at least fifteen minutes to avoid surface glazing.
Clearance: the high clutch applies while the low band releases, so shift overlap timing matters. Rest the flat bar of a vernier caliper or depth micrometer on the sun gear flange ledge (about 3/16” below the top snap ring groove) and extend the rod to the top friction plate. Total clutch pack clearance should be .080 +/- .010, within a minimum/maximum of .060-.100. An aftermarket front clutch hub is recommended so all of the kit's contents can be installed.
What's included
- (8) 019742-155 Red Eagle® friction plates with external teeth, .061” / 1.55mm
- (7) 019731K155 Kolene® steel plates with internal teeth, .060” / 1.52mm
- (1) 019701AK Kolene® steel plate with external teeth, .060” / 1.52mm
Notes
In order to install the full capacity of eight (8) friction plates, a V-8 clutch drum must be used.
Additionally, the clutch drum piston must be machined (a simple procedure) and the waved cushion plate is not reinstalled.
Using a ruler or vernier caliper, measure from the bottom of the clutch drum to the ledge where the sun gear flange rests.
Using a vernier caliper or micrometer, measure equal distances from the three (3) individual piston pads to the top of the piston depicted in the illustration between the two horizontal lines as area “A”.
An OEM V-8 piston will measure approximately .860”.
Important Note: DO NOT machine the piston below .740”.
ALWAYS check the proximity of the first steel plate to ensure that the plate lugs are in the lugs of the clutch drum.
You will NOT be installing a waved cushion plate.
Refer to the illustrations to measure the overall clutch pack clearance.


